Blog
When to Automate a Manual Valve: Build the Decision Record
12 November 2026
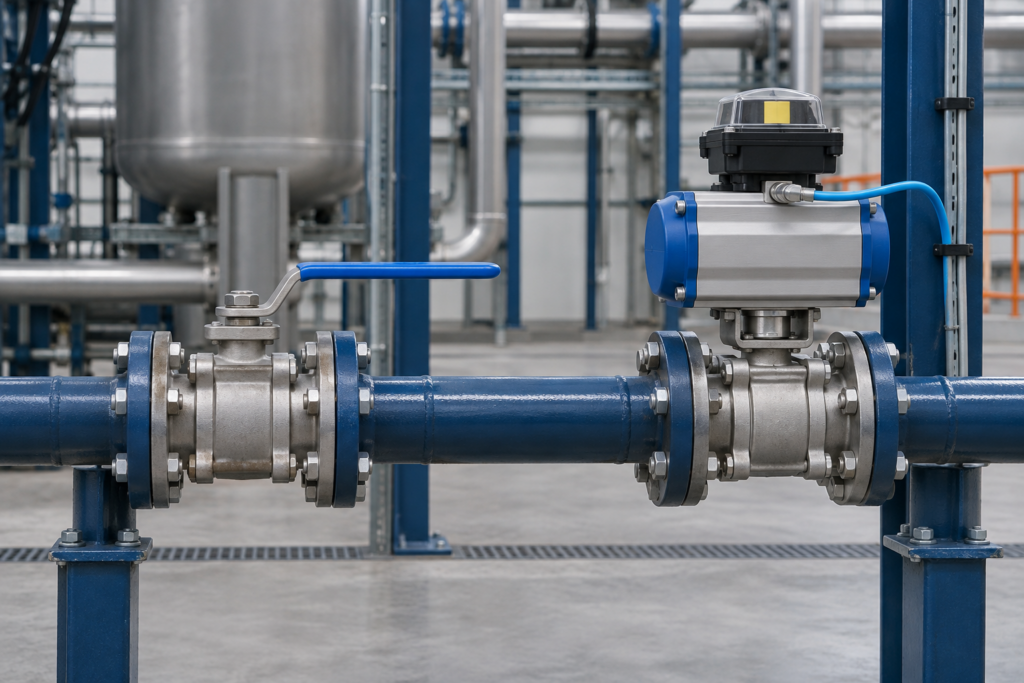
Automating a manual valve can make sense when the required operating function cannot be delivered consistently, promptly or safely from the handwheel or lever. It can also add cost, utilities, controls, failure modes and maintenance tasks that a simple manual valve does not have.
The useful question is therefore not whether automation is generally better. It is whether a defined valve duty justifies a complete actuator and control package. This guide provides a decision record for that comparison without assuming a generic payback.
Quick answer
Consider valve automation when a clearly defined function needs remote, automatic, interlocked or repeatable operation; when access or response time makes local operation unsuitable; or when position feedback is required. Before committing, record the valve duty, operating frequency, required travel and time, available power or instrument air, control signal, failure response, environment, feedback, maintenance and commissioning route. Compare the complete package with the existing manual task using site data rather than a generic savings claim.
Start with the function, not the actuator
A manual valve may be entirely appropriate for an infrequent, accessible and procedurally controlled task. Automation needs a specific reason. That reason might be normal sequence control, remote isolation, modulation, a required response time, operation from a safe location, position confirmation or integration with an existing control system.
The Health and Safety Executive’s guidance on remotely operated shut-off valves uses a risk-assessment process to decide whether remote operation is needed for hazardous-substance isolation. It does not treat remote actuation as a universal upgrade. HSE control-system guidance likewise treats valves, actuators, positioners, utilities and control logic as parts of the complete function. Those principles support a structured record even where the proposed valve is not part of a safety instrumented system.
Seven checks before converting a manual valve
1. Define the required operating function
Write the function in one sentence. Examples include open or close on an operator command, move to a defined position in a process sequence, modulate to a control signal, isolate from a remote station, or report confirmed end position. Do not use “improve automation” as the requirement.
Separate normal process control from an emergency or protective function. HSE notes that control, isolation and safety functions have different requirements and that a control valve should not be assumed to provide isolation. If risk reduction is being claimed, the complete safety lifecycle, integrity, testing and competence requirements need assessment by the responsible engineering team.
2. Record access, exposure and response
Observe the existing task. Record where the operator stands, how the valve is reached, what permits or access equipment are required, how long the full operation takes, how the position is confirmed and what happens during an upset. HSE pressure-system guidance says equipment should be operable without having to climb or struggle through pipework or structures, but an awkward location alone does not specify the actuator package.
Where remote isolation is proposed, record who initiates it, where the command point sits, how a release or abnormal condition is detected and what response is required. These are application facts, not benefits that can be inferred from the actuator catalogue.
3. Measure the real operating demand
Count operations over a representative period and separate routine cycles, start-up and shutdown movements, testing, maintenance and abnormal demands. Record whether the valve must stop mid-travel, how quickly it must move and whether simultaneous valve movements could affect the process or utility supply.
No universal number of operations proves that automation will pay back. Frequency matters because it shapes wear, energy or air consumption, operator demand and maintenance, but the decision needs the site’s own baseline.
4. Confirm the valve can be automated
Identify the exact valve, size, pressure and temperature duty, materials, mounting interface, stem or shaft dimensions, travel, direction and required torque or thrust across the full stroke. Include break, running and seating requirements where applicable, plus the manufacturer’s maximum allowable stem or shaft load.
An actuator should not be selected from nominal valve size alone. The proposed mounting kit, coupling, travel stops and any manual override form part of the mechanical package. If the existing valve lacks reliable current data or a suitable interface, replacing the valve and actuator as an engineered assembly may be a different decision from retrofitting the actuator.
5. Map utilities, controls and environment
For a pneumatic route, record minimum available pressure at the actuator during the worst simultaneous demand, air quality, tubing, filter regulator, solenoid arrangement and exhaust requirements. For an electric route, record supply, current, control type, duty cycle, local controls and isolation. For either route, record ambient temperature, weather exposure, washdown, corrosion, vibration and any hazardous-area classification.
Emerson’s valve-operating-system description shows why the boundary extends beyond the actuator: a packaged solution can include air preparation, relief devices, solenoids, limit switches, positioners, tubing, engineering and maintenance documents. The necessary components still depend on the application; the list is not a universal specification.
6. Define failure behaviour, feedback and safeguards
State what should happen on loss of air, electrical supply, command signal or communications. The required result may be stay put, spring to a defined position, move using stored energy or remain available for controlled manual operation. The process consequence decides the answer.
Record how open, closed and fault states will be indicated, what local and remote commands are allowed, how unexpected movement is prevented during maintenance, and how overrides and resets are controlled. HSE identifies actuator reliability, utilities, end-position monitoring, testing and failure behaviour as parts of control-system integrity. A feedback switch proves a switch state; it does not by itself prove process isolation.
7. Plan commissioning and lifecycle support
Define inspection, functional test and acceptance criteria before purchase. Include direction of travel, end stops, indication, control commands, loss-of-utility response, manual override, interlocks, timing where relevant and post-maintenance reinstatement. Keep the current drawings, instructions and settings with the asset record.
Automation changes the maintenance scope. The valve still needs attention, and the actuator, mounting, accessories, utilities and controls add inspection and test tasks. HSE guidance treats design, validation, installation, commissioning, operation, maintenance and modification as a lifecycle rather than a one-off hardware purchase.
Build a site-specific value case
A defensible value case compares the current manual task with the proposed complete package over an agreed period. Keep observed facts separate from estimates.
| Record | Manual baseline | Automation proposal | Evidence |
|---|---|---|---|
| Required result | Local action and current confirmation method. | Remote, automatic, interlocked or modulating function. | Operating philosophy and risk or process assessment. |
| Operating demand | Observed operations, travel time and access steps. | Expected cycles, movement time and sequence. | Dated task observation and control narrative. |
| People and access | Permits, access equipment and exposure controls. | Remaining local tasks and remote operating point. | Task assessment and layout. |
| Installed scope | Existing valve and maintenance. | Valve, actuator, mounting, accessories, utilities, controls and commissioning. | Comparable quotations and drawings. |
| Lifecycle | Inspection, lubrication, packing, seats and manual operation. | All valve tasks plus actuator, accessory, utility, test and spares tasks. | Manufacturer instructions and site maintenance plan. |
| Operational consequence | Current response, variability and process effect. | Expected response and new failure modes. | Process data, risk review and acceptance test. |
Use approved local labour, downtime, energy, compressed-air, maintenance and capital assumptions if a financial appraisal is required. Record the source and sensitivity of each figure. This article does not provide a universal payback period.
What to send for an automation review
- Valve manufacturer, model, size, connection, materials and current photographs or drawings.
- Medium, pressure, temperature and normal operating conditions.
- Required function: on/off, modulating, sequencing, remote isolation or position indication.
- Operating frequency, travel-time requirement and current access method.
- Available electrical supply or minimum instrument-air pressure and quality.
- Required failure position or behaviour, with the process reason.
- Control signal, feedback, local controls, interlocks and communications.
- Environment, hazardous-area needs, ingress protection and corrosion exposure.
- Torque or thrust evidence, mounting details and allowable stem or shaft loads.
- Testing, documentation, spares and maintenance requirements.
Review the current Valves4You actuator range, or send the duty through the contact route. The industry pages provide additional application context.
Frequently asked questions
How many valve operations justify automation?
There is no universal threshold. Record actual frequency, task time, access controls, process need, installed scope and lifecycle work. A rarely operated valve may still need remote action for a defined risk or process reason, while a frequently used accessible valve may remain manual.
Does automating a valve automatically make the task safer?
No. Remote operation may change operator exposure, but it also introduces power, controls and unexpected-movement risks. Assess the complete task, process consequence and maintenance isolation arrangements.
Can an actuator be fitted to any existing valve?
No. Confirm the valve condition, torque or thrust across the stroke, mounting interface, stem or shaft strength, travel, direction and manufacturer limits. Some retrofits need a purpose-designed mounting kit; others are better handled as a new valve-and-actuator assembly.
Should a valve fail open or fail closed?
The process consequence decides. Loss of power, air, signal and communications should each be considered. The answer may also be fail in place or a controlled stored-energy action. Do not choose from habit.
Is position feedback the same as proof of isolation?
No. A limit switch or position transmitter reports the state it is designed to detect. It does not by itself prove seat leakage performance or process isolation.
Talk to Valves4You about your application
For a valve-automation review, send the exact valve details, duty, operating frequency, required function, available utilities, control and feedback needs, environment and failure response. Valves4You can then compare actuator and package routes against the recorded requirement without assuming a generic payback.